How to Calculate OEE: Formula, Worked Example and the Six Big Losses
OEE = Availability × Performance × Quality. A step-by-step calculation with a worked example, the six big losses, benchmarks and the mistakes that skew OEE.
Key takeaways
- OEE (overall equipment effectiveness) = Availability × Performance × Quality. It shows how much of your planned production time made good parts at full speed.
- Shortcut: OEE = (Good count × Ideal cycle time) ÷ Planned production time.
- Worked example in this guide: 90% availability × 88.9% performance × 95% quality = 76% OEE.
- 85% is the commonly cited world-class figure, but a machine's trend against itself, and its biggest loss, matter more than any benchmark.
What OEE measures
Overall equipment effectiveness (OEE) is the share of planned production time that was truly productive: making good parts, as fast as the machine is designed to run, without stopping. An OEE of 100% means only good parts, at ideal speed, with no downtime.
Seiichi Nakajima developed OEE in Japan as part of total productive maintenance (TPM). It is popular because it splits every lost minute into three plain questions:
- Availability: was the machine running when it should have been?
- Performance: when it ran, did it run at full speed?
- Quality: of what it made, how much was good the first time?
The OEE formula
Multiply the three and most terms cancel out, which gives a useful shortcut and a good cross-check:
The terms, in plain words:
| Term | What it means |
|---|---|
| Planned production time | The time the machine was scheduled to produce: shift length minus planned breaks and time with no orders. |
| Downtime | Stops during planned production time: breakdowns, changeovers, adjustments, waiting for material. |
| Run time | Planned production time minus downtime. |
| Ideal cycle time | The fastest time to make one part under ideal conditions, often the design or nameplate speed. |
| Total count | Everything the machine made, good and bad. |
| Good count | Parts that were right the first time, with no rework. |
Worked example: one 8-hour shift
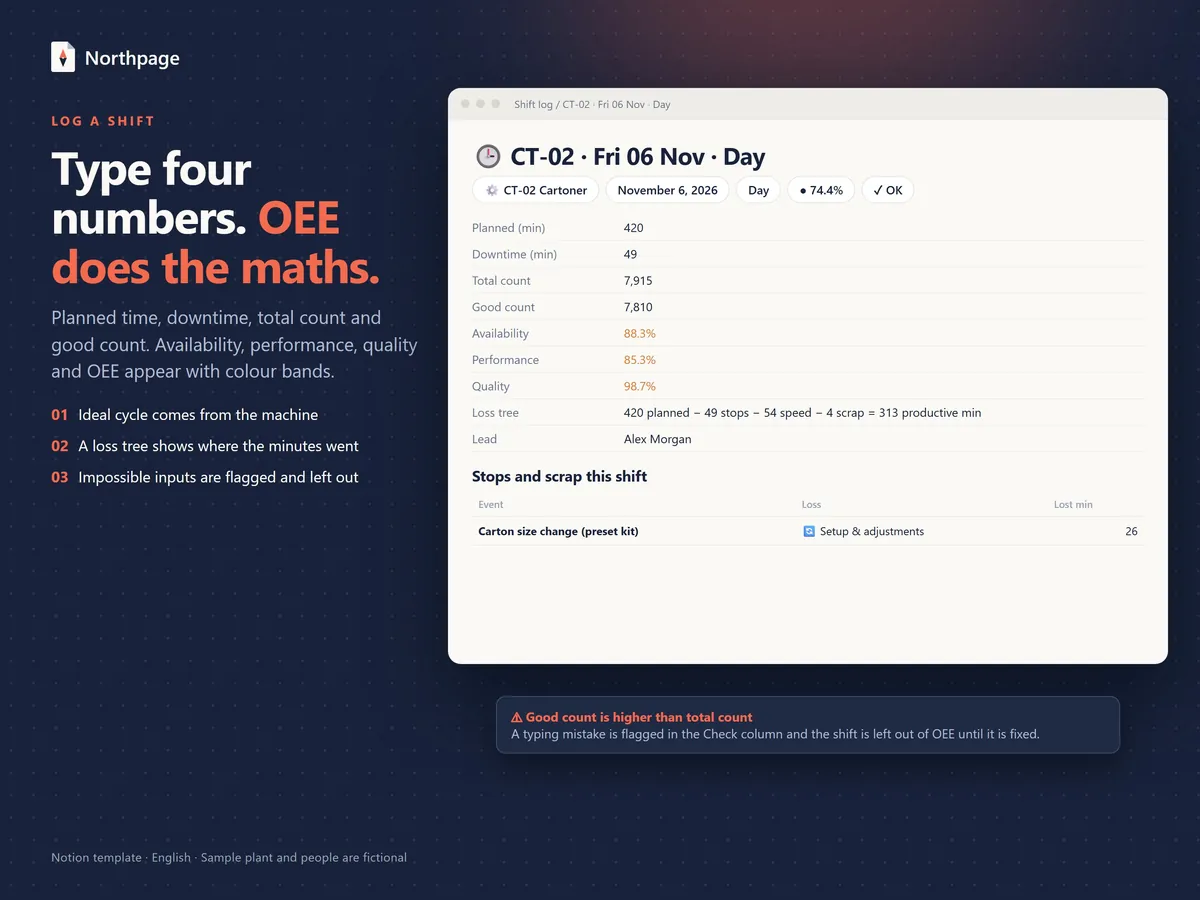
A carton packing machine runs an 8-hour shift (480 minutes) with a 30-minute break. During the shift it has a 25-minute breakdown and a 20-minute changeover. Its ideal cycle time is 30 seconds (0.5 minutes) per carton. It packs 720 cartons, and 36 of them are rejected.
| Input | Value |
|---|---|
| Planned production time | 480 − 30 = 450 min |
| Downtime | 25 + 20 = 45 min |
| Run time | 450 − 45 = 405 min |
| Ideal cycle time | 0.5 min per carton |
| Total count | 720 cartons |
| Good count | 720 − 36 = 684 cartons |
Now the three factors:
Check it with the shortcut: (684 × 0.5) ÷ 450 = 342 ÷ 450 = 76.0%. Same answer.
Where did the other 24% go?
Turning each loss into minutes shows where to look first:
| Loss | Minutes | How it is worked out |
|---|---|---|
| Availability loss | 45 | The breakdown plus the changeover |
| Performance loss | 45 | 405 minutes of run time minus the 360 minutes the 720 cartons should have taken |
| Quality loss | 18 | 36 rejects × 0.5 minutes each |
| Fully productive time | 342 | 450 − 45 − 45 − 18 = 342, which is 76% of 450 |
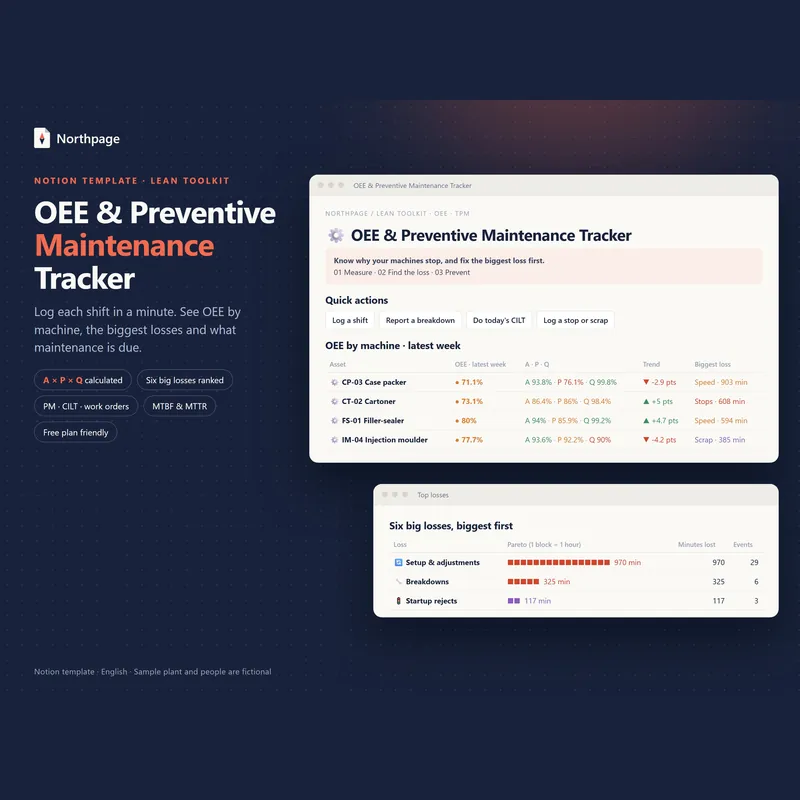
Availability and performance cost the same here: 45 minutes each. The performance loss is the easy one to miss, because the machine was running the whole time. Short stops and a slower speed add up without anyone writing them down.
The six big losses
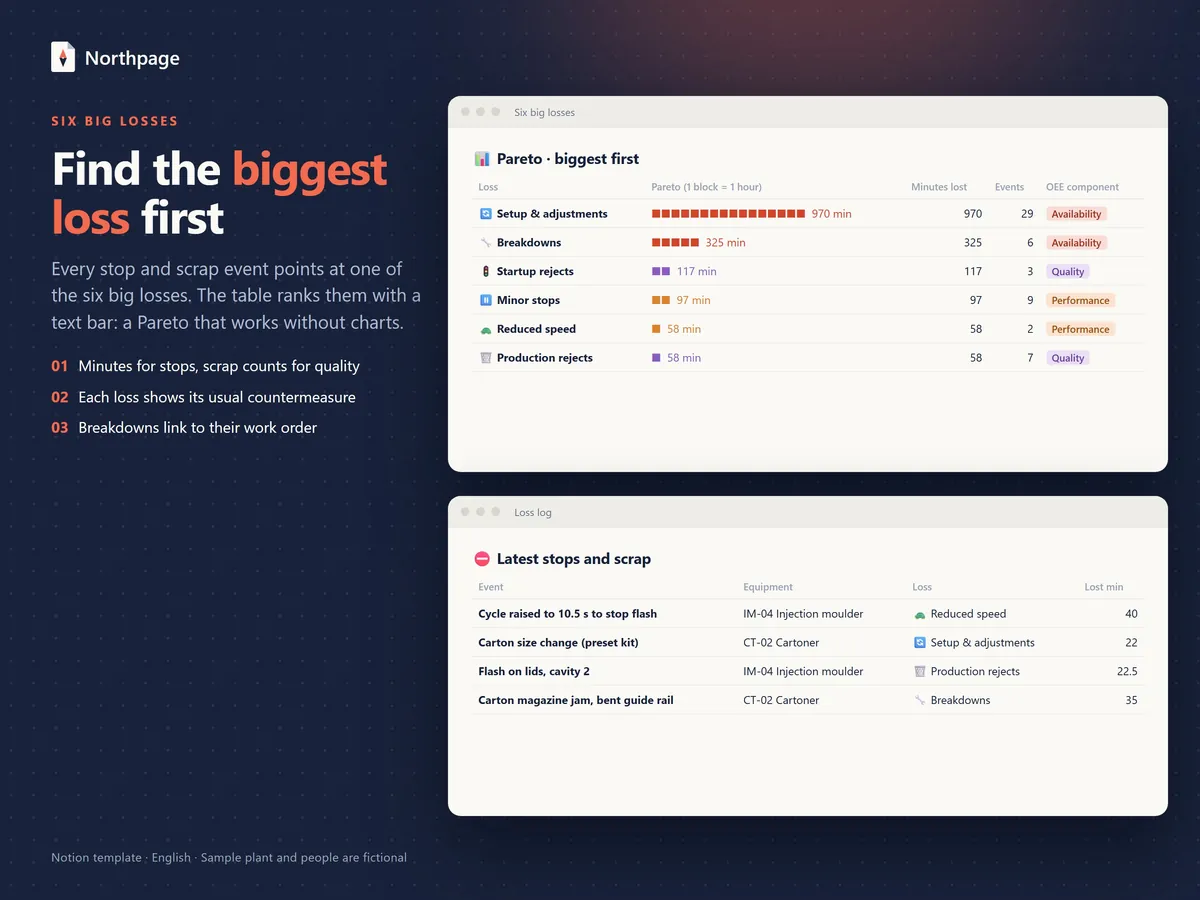
TPM sorts every loss into six groups, two for each OEE factor. Logging each stop or reject against one of them tells you which loss is biggest, so you know what to fix first.
| OEE factor | Loss | Examples |
|---|---|---|
| Availability | Breakdowns | Motor failure, a jammed feeder, broken tooling |
| Availability | Setup and adjustments | Changeovers, warm-up, first-part adjustments |
| Performance | Minor stops | Short jams, sensor trips, a blocked or starved conveyor, usually under 5 minutes each |
| Performance | Reduced speed | Running below ideal speed because of wear, material or a cautious setting |
| Quality | Startup rejects | Scrap and rework while the process settles after a start or changeover |
| Quality | Production rejects | Scrap and rework during steady running |
What is a good OEE score?
The commonly cited world-class OEE is 85%, from 90% availability × 95% performance × 99.9% quality. These figures are often quoted as rules of thumb:
- 100%: perfect production. Only good parts, at ideal speed, with no stops.
- 85%: world class for discrete manufacturing.
- About 60%: typical.
- About 40%: low, but common when a plant first starts measuring.
Treat them as a rough guide. A machine with long changeovers by design, or a process with strict quality demands, will sit at a different level. The useful comparison is a machine against its own history, week by week, together with the loss that costs it the most minutes.
Common OEE mistakes
- Using the average cycle time instead of the ideal one. Performance then hides your speed losses. Use the design speed, or the best speed you have sustained.
- Leaving changeovers out of downtime. Setup time is a real loss and one of the six. Only planned breaks and time with no orders come out of planned production time.
- Counting rework as good. Good count means right the first time.
- Averaging OEE percentages across machines. A simple average gives a 10-minute trial run the same weight as a full shift. Weight each machine or shift by its planned production time.
- Accepting performance over 100%. That can't happen; it means the ideal cycle time is set too slow.
- Chasing the number instead of the losses. OEE tells you how much you lose. The loss log tells you why.
How to calculate OEE in Excel or Google Sheets
Put one shift per row: planned production time in column A, downtime in B, ideal cycle time in C (in the same unit as A, for example minutes), total count in D and good count in E. Then add these formulas in row 2:
Format F to J as percentages; columns I and J should always match. To roll several shifts or machines up, add up the time and count columns first and then apply the same formulas, instead of averaging the percentages.
A spreadsheet is a fine start. It gets harder once you want every stop logged against one of the six big losses, MTBF and MTTR per machine, and preventive maintenance in the same place.
OEE, MTBF and MTTR
Breakdowns hit availability, and two reliability figures show whether they are getting better:
A rising MTBF means breakdowns are getting rarer; a falling MTTR means they are fixed faster. Preventive maintenance and daily clean, inspect, lubricate and tighten (CILT) checks push MTBF up, which lifts availability and OEE with it. A clean, well-organized machine area helps too: see our guide to 5S and the 5S audit.
Frequently asked questions
What is the formula for OEE?
OEE = Availability × Performance × Quality, where Availability = Run time ÷ Planned production time, Performance = (Ideal cycle time × Total count) ÷ Run time, and Quality = Good count ÷ Total count. The shortcut OEE = (Good count × Ideal cycle time) ÷ Planned production time gives the same result.
What is a good OEE score?
85% is widely quoted as world class for discrete manufacturing, about 60% as typical, and about 40% as common when a plant first starts measuring. The most useful comparison is a machine against its own history.
What is the difference between OEE and TEEP?
OEE measures losses during planned production time. TEEP (total effective equipment performance) measures against all the time there is, 24 hours a day, 7 days a week: TEEP = OEE × Utilization, where Utilization = Planned production time ÷ All time.
Can OEE be more than 100%?
No. If performance comes out above 100%, the ideal cycle time you used is slower than what the machine can really do. Correct it to the true ideal speed.
Does planned maintenance count as downtime in OEE?
If the maintenance happens during time you planned to produce, yes: count it as downtime (a planned stop). If you schedule it outside planned production time, it doesn't lower OEE, though it does lower TEEP.